
Low Pressure Permanent Mold Casting: When the Fill Method Matters
Low pressure permanent mold uses the same kind of steel die as tilt pour, but the metal comes in from underneath. The die sits over a sealed furnace, and a small amount of air pressure pushes molten aluminum up a fill tube into the cavity. The fill is slow, controlled, and free of the turbulence that comes with pouring, and the pressure is held while the casting solidifies so metal keeps feeding it from below.
How low pressure casting works
- Melt and hold. Aluminum is held at pouring temperature in a sealed, pressurized furnace beneath the die.
- Close the die. Steel cores and any sand cores are set, the die closes, and the riser tube connects the furnace to the bottom of the cavity.
- Pressurize. Air pressure in the furnace is raised gradually, typically 0.3 to 0.7 bar (about 4 to 10 psi) and rarely above 15 psi, pushing metal up the tube and into the cavity at a programmed rate. The metal front rises smoothly with no free surface tumbling.
- Hold and feed. Pressure is maintained while the casting solidifies. As the metal shrinks, more is pushed in from below, so the casting freezes from the far walls back toward the tube and shrinkage ends up in the tube, not the part.
- Release and eject. Pressure is released, unsolidified metal in the tube drains back to the furnace, the die opens, and the casting is ejected. There is very little gating to remove.
- Heat treat, machine, inspect. T6 heat treatment, machining, and inspection follow in the same building.
The name comes from the pressure being low, a small fraction of what high pressure die casting uses. What matters is control rather than force: the fill rate is set precisely, the metal never splashes, and the feed continues until the casting is solid.
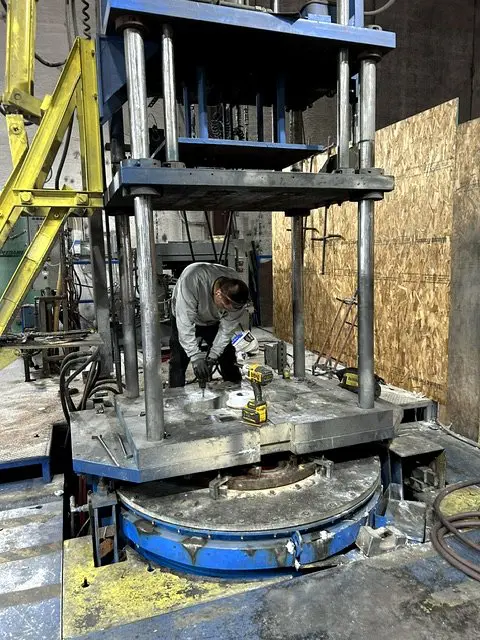
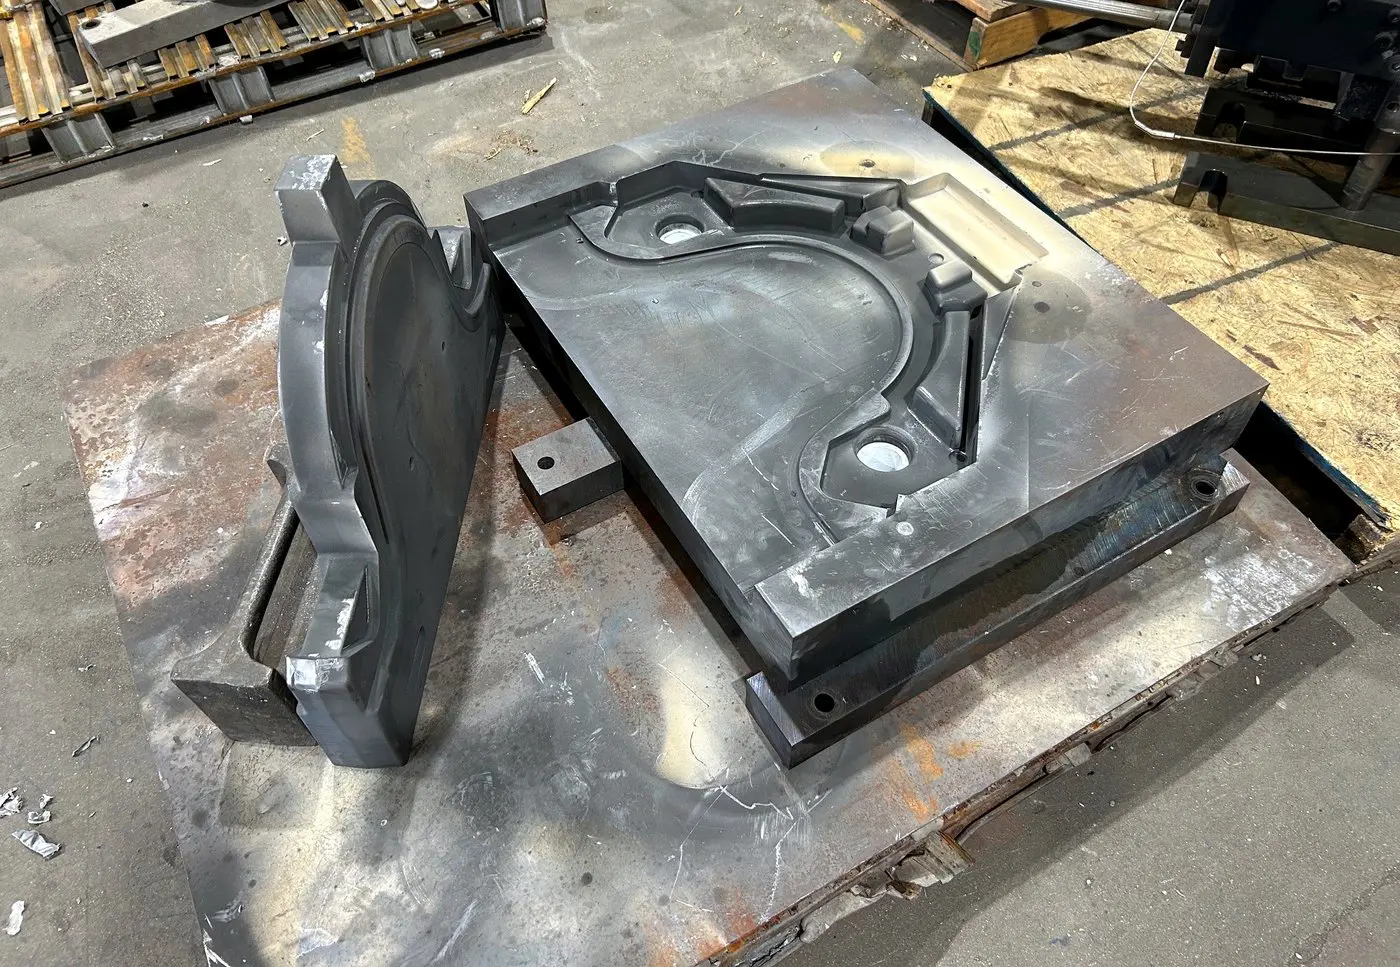
Left: a low pressure machine at Protocast, with the pressurized holding furnace under the die. Right: a low pressure die with a slide, cut in the Protocast tool room.
What low pressure adds over tilt pour
- Thin walls. Gravity fills moderate walls well, but the metal front slows as it climbs and spreads into thin sections, and the last areas to fill can freeze short. Pressure keeps the front moving and fills walls that gravity cannot.
- Heavy sections. A large boss or thick flange solidifies last and pulls metal from around it. Continuous feed pressure keeps that section sound without oversized risers.
- Soundness. A bottom-up, non-turbulent fill traps less air and folds in less oxide, which matters on pressure-tight and structural parts and on anything that will be x-rayed.
- Yield. Very little gating, and the riser tube drains back to the furnace, so more of the metal poured ends up in the part and there is less to trim and remelt.
- Rate. A low pressure part runs at roughly 40 pieces an hour against about 50 for tilt pour, so the piece price is a little higher. The volume range is the same as tilt pour, roughly 300 to 50,000 pieces a year.
What to expect
| Item | Typical at Protocast |
|---|---|
| Annual volume (EAU) | Roughly 300 to 500 pieces a year up to about 50,000, the same as tilt pour |
| Tooling | Steel die designed for bottom fill, about 40,000 shots before refurbishment |
| Surface finish | 125 to 250 rms |
| Minimum wall | Typically 0.125 inch; low pressure makes the thin end of that range achievable over larger areas |
| Tolerances | Aluminum Association Standards for Aluminum Sand and Permanent Mold Castings |
| Alloys | Aluminum, including 356 and 357, heat treated to T6 in house |
| Sample lead time | Typically 12 to 20 weeks for raw castings from a new die |
| Tooling cost | $35,000 to $200,000 depending on size and complexity, most under $100,000; cut in house whenever possible; customer owned |
Figures are typical and depend on geometry and workload.
Low pressure, gravity, and high pressure: three different things
The names cause more confusion than the processes. All three use steel dies, which is why “die casting” gets attached to each of them, but the fill method decides the tooling, the volumes, and the properties.
| Tilt pour (gravity) | Low pressure | High pressure die casting | |
|---|---|---|---|
| Fill | Gravity, die rotates | Pushed up from below at roughly 4 to 10 psi | Injected at very high pressure |
| Fill speed | Controlled | Slow and programmed | Milliseconds |
| Trapped gas | Low | Lowest | Highest |
| Heat treatable | Yes | Yes | Generally no |
| Thin walls | Moderate | Good | Best |
| Tooling cost | Moderate; $35,000 to $200,000 | Moderate; same range as tilt pour | Highest |
| Volume | 300 to 50,000 | 300 to 50,000 | Usually 50,000 to 100,000 and up in North America |
| Rate | About 50 an hour | About 40 an hour | Fastest; robotic trim and handling |
| At Protocast | In house | In house | Offered |
If a drawing or a purchase order says “low pressure die casting,” it means this process. If it says “die casting” without qualification, ask which one is meant; the tilt pour versus low pressure guide is written to help settle that conversation.
Parts that suit low pressure
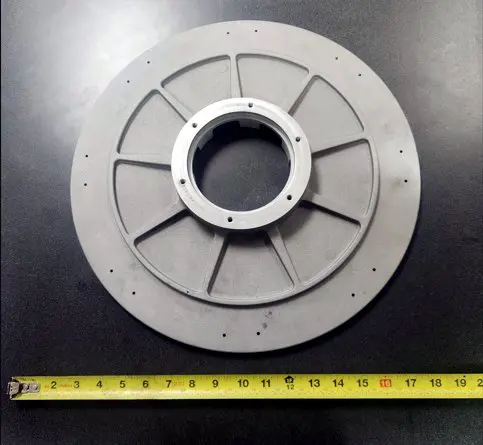
Thin-wall housings and enclosures, pressure-tight manifolds and pump bodies, wheels and structural parts with heavy hubs and thin webs, heat sinks with fine fins, and any casting that will be pressure tested or radiographed. Industries that specify it include automotive, aerospace, defense, fluid power, and industrial equipment. The thin-wall housing guide and the pressure-tight casting guide go deeper on the two most common reasons parts come to this process.
Designing for low pressure
The permanent mold design rules apply: uniform walls, draft on every vertical face, radii on inside corners, machining stock on critical faces. Two things are specific to low pressure. The riser tube location is designed with the part, and features that would block the rising metal front need attention early. And because the casting freezes from the top and far walls back toward the tube, the heaviest sections should sit closest to the tube where feed pressure reaches them last. The DFM review and the flow simulation at the quote stage settle both.
Common defects and how they are prevented
| Defect | Cause | Prevention |
|---|---|---|
| Misrun in thin walls | Fill too slow or die too cold | Pressure ramp and die temperature set from simulation |
| Shrinkage in heavy sections | Section isolated from feed | Heavy sections placed toward the tube; hold pressure until solid |
| Oxide inclusions | Turbulent fill | Programmed, non-turbulent fill rate; clean melt |
| Tube-related defects | Metal freezing in the riser tube | Tube temperature control and timing |
| Dimensional drift | Die wear and temperature swing | Temperature control, coating practice, scheduled refurbishment |
When to choose it over tilt pour
If the part has thin walls, a heavy boss or flange, or a pressure requirement, low pressure is usually the answer. If the walls are thicker and gravity alone will fill the cavity, tilt pour runs a little faster and costs a little less per piece. Volume does not decide it; both processes cover the same range. When it is not obvious, the flow simulation at the quote stage usually settles it, and if a part can be made either way, Protocast quotes the process that is most economical for the customer.
Terms you will see
- LPDC
- Low pressure die casting, the common industry name for this process.
- Riser tube / stalk
- The tube connecting the furnace to the bottom of the die through which metal rises.
- Pressure ramp
- The programmed increase in furnace pressure that sets the fill rate.
- Holding pressure
- Pressure maintained after fill so metal keeps feeding the casting as it solidifies.
- Directional solidification
- Freezing that proceeds from the far end of the casting back toward the feed, so shrinkage is pushed out of the part.
- Yield
- The share of metal poured that ends up in the finished casting rather than in gating.
How Protocast fits in
Protocast runs low pressure in house on its own equipment, one machine daily with a second being brought into service, alongside its tilt pour machines, so the recommendation on fill method is made on the part rather than on which machine happens to be available. Send the model with the annual quantity and the wall thicknesses you are worried about; the simulation will show whether gravity fills them or whether the part needs pressure, and the quote will say which and why.
Frequently asked questions about low pressure casting
What is low pressure permanent mold casting?
A permanent mold process in which molten aluminum is pushed up into a steel die from a pressurized furnace beneath it, at roughly 4 to 10 psi, and held under pressure while it solidifies.
Is low pressure die casting the same as low pressure permanent mold?
Yes. Both names describe a steel die filled from underneath by low air pressure. The name differs by region and industry; the process does not.
How is it different from high pressure die casting?
High pressure die casting injects metal in milliseconds at very high pressure into a different style of die with much higher tooling cost and larger minimum volumes. Low pressure fills gently from below, which gives better soundness and mechanical properties, allows heat treatment, and makes sense at lower volumes.
What is the minimum wall thickness?
Typically 0.125 inch in permanent mold. Low pressure makes the thin end of that range easier to fill over large areas, and exceptions are possible depending on geometry.
What volumes suit low pressure?
The same as tilt pour: from roughly 300 to 500 pieces a year up to about 50,000. The part decides between the two processes, not the quantity.
Are low pressure castings heat treated?
Yes. Like all permanent mold castings at Protocast, they are heat treated to T6 in house, typically within 2 to 3 days of casting.
What alloys are used?
Aluminum casting alloys, principally 356 and 357. Chemistry is verified on an in-house spectrometer.
Does low pressure produce a better surface than tilt pour?
The as-cast finish is the same range, 125 to 250 rms, because both come from a coated steel die. Low pressure’s advantage is internal soundness, not surface.
Can low pressure castings be pressure tested?
Yes, and the process is often specified for exactly that reason. Pressure and leak testing is available to customer-defined procedures.
Send the model. Get a quote with engineering feedback.
Have a thin-wall or pressure-tight part? Send the model and we will show you whether low pressure is needed.
- Engineering review with every quote
- Flow simulation before tooling is cut
- Cast, heat treated, machined, and inspected in one building
- Permanent mold tooling cut in house whenever possible
