
Casting Resources
Practical guides on permanent mold, low pressure, tilt pour, and sand casting for engineers and buyers sourcing aluminum and zinc castings, from the Protocast foundry in Commerce City, Colorado.
Permanent Mold Casting
The production process and the umbrella for everything below it. Steel tooling, consistent geometry, and a per-part price that drops as volume climbs.
Start hereLow Pressure Permanent Mold
Also called low pressure die casting. The alloy is pushed up into the die from underneath, which fills thinner walls that gravity cannot. Same volume range as tilt pour; the part decides which.
Start hereTilt Pour / Gravity Permanent Mold
The most common way to fill a permanent mold, and the process buyers search for as gravity die casting or gravity permanent mold.
Start hereSand Casting & Printed Sand
Where most programs begin. Precision no-bake sand for fast first parts, and printed sand molds for complex geometry with no tooling at all.
Start hereReal Parts, Real Volumes
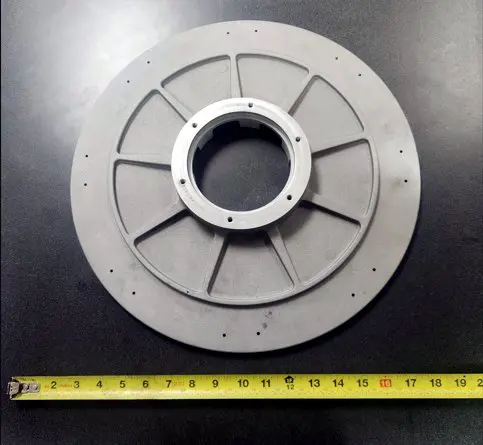
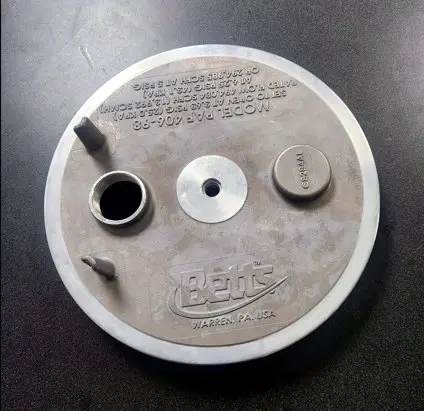
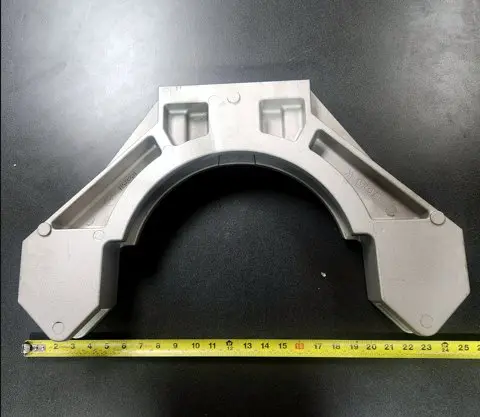
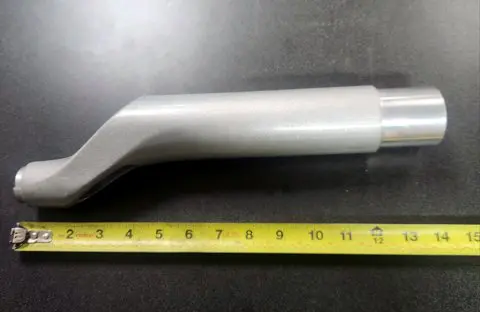
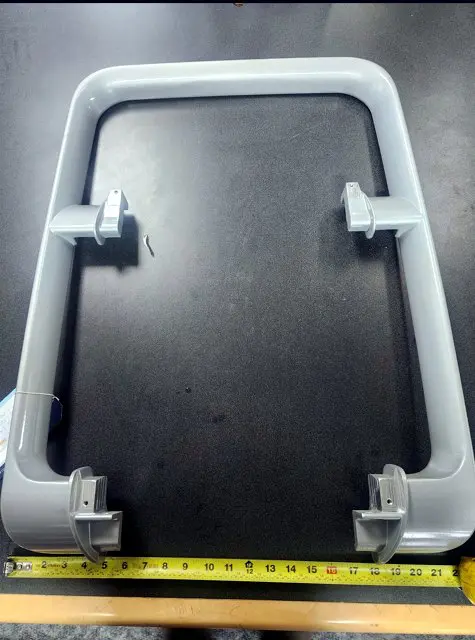
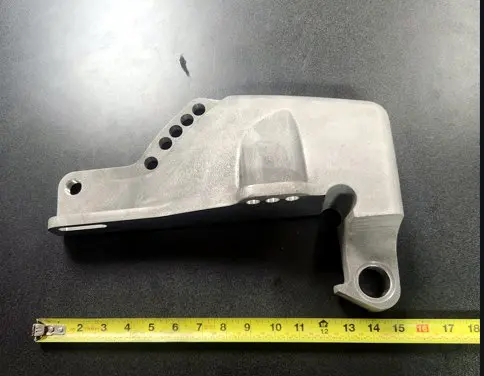
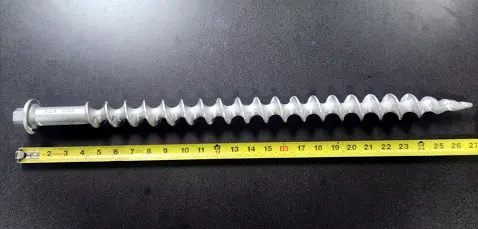
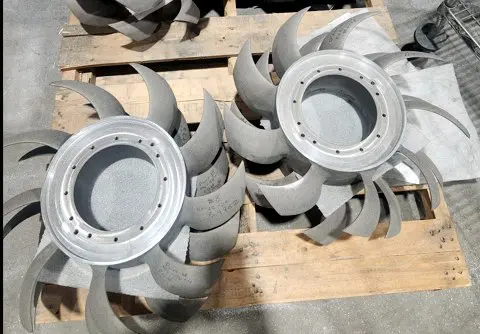
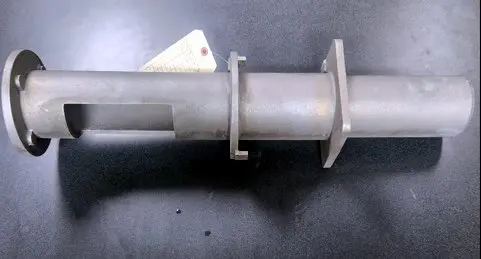
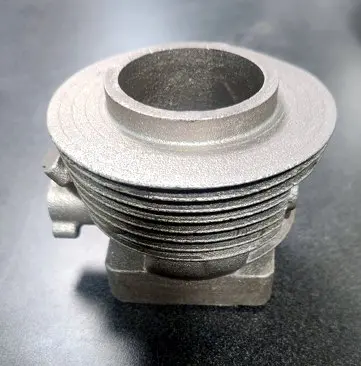
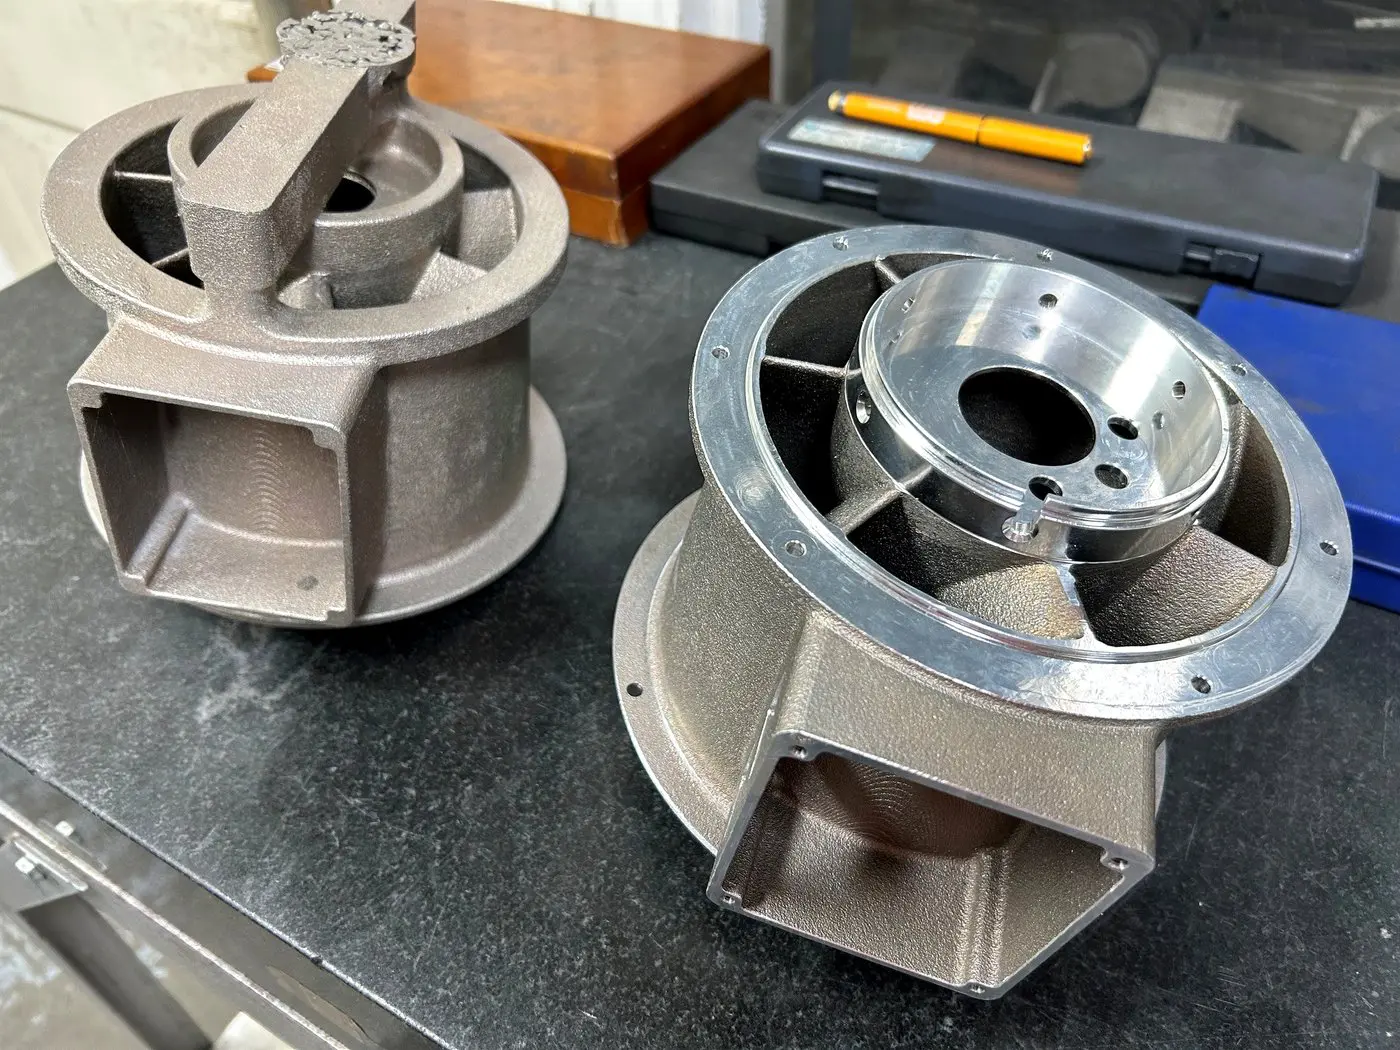
A few castings Protocast produces, with the process each one runs in and the annual volume behind it. The pattern is the point: printed sand and precision sand carry the low numbers, permanent mold carries the thousands, and the part decides between tilt pour and low pressure.
Answers and Reference
The numbers we quote from and the pages that support every process above.
Talk to a Protocast engineer.
Whether it is a process question, a quote, or a part that needs to move from prototype to production, the engineering team works from these same questions every day. Send the model and you will get a process recommendation, DFM feedback, and in most cases a flow simulation check with the quote.
